Quick Answer: A dial gauge is a comparative measuring instrument that displays small linear variation on a graduated circular dial. A spring-loaded spindle moves against the part, and an internal gear train amplifies that movement into pointer travel. It measures runout, flatness, parallelism and dimensional deviation against a reference.
What is a Dial Gauge?
What is a dial gauge? A dial gauge, also called a dial indicator, is a precision instrument that measures small linear displacement. A spindle or lever moves against the workpiece, and a gear train converts that movement into pointer rotation on a graduated dial. It is used for runout, flatness, alignment and comparative height checks.
A dial gauge measures change rather than absolute size. It compares a feature against a set zero or a master.
The instrument is also called a dial indicator. It is a core tool in quality control, toolrooms and inspection.
Engineers use it to check how much a surface deviates from a target. The dial makes very small movement easy to read.
A dial gauge measures small linear displacement by converting plunger movement into pointer rotation.
How Does a Dial Gauge Work?
How does a dial gauge work? A dial gauge works on a rack and pinion principle. When the plunger moves, a rack on the spindle turns a pinion, and a gear train magnifies the motion onto the main pointer. A revolution counter tracks full turns, so small travel becomes an easily read dial value.
The contact point touches the part through a spring-loaded spindle. The spring keeps a steady measuring force.
As the spindle moves, a rack and pinion or gear train turns the pointer. This mechanism amplifies tiny movement into a clear dial reading.
The outer bezel rotates so the operator can set zero. Each pointer division then shows a fixed unit of displacement.

Least Count: The least count of a dial gauge is the smallest value one dial division represents. A common metric dial gauge has a least count of 0.01 mm — each small division equals one hundredth of a millimetre. Always confirm the least count printed on the specific instrument.
The rack and pinion mechanism inside a dial gauge magnifies small movements onto a readable dial.
Dial gauge diagram and parts name
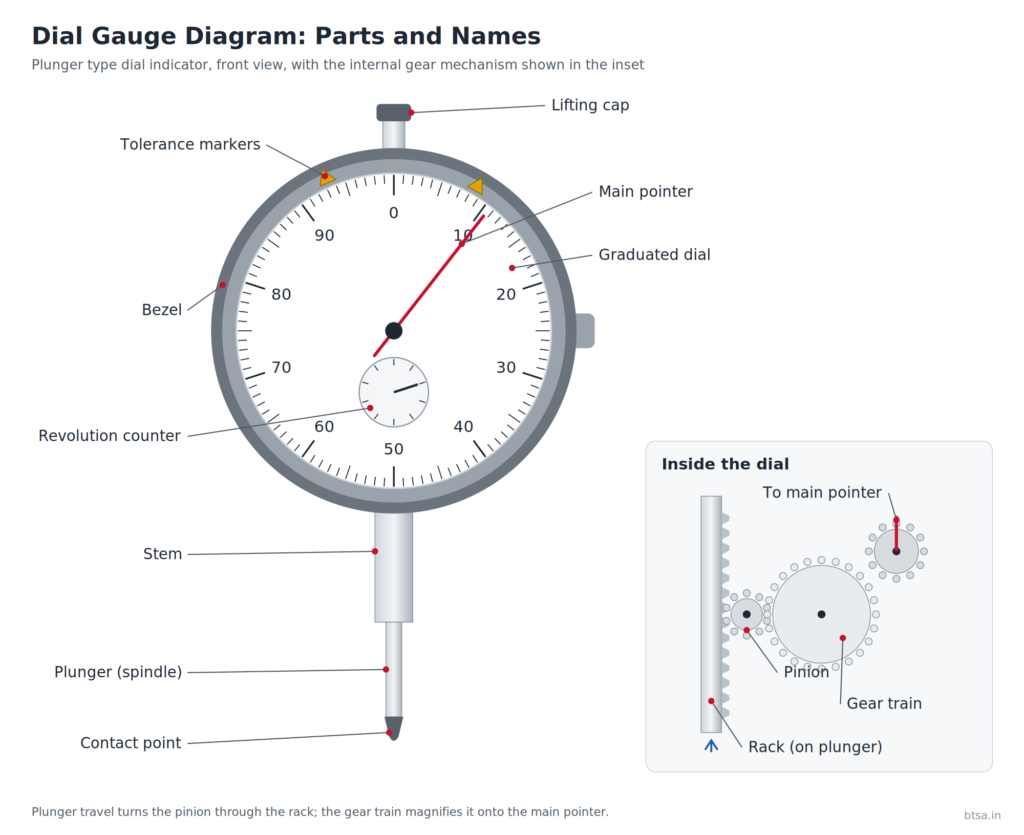
| Part | Function |
|---|---|
| Plunger (spindle) | Moves in and out as it contacts the workpiece |
| Contact point | Tip that touches the surface; interchangeable |
| Stem | Mounting shank for stands and fixtures |
| Rack and pinion | Converts straight plunger travel into rotation |
| Gear train | Magnifies rotation onto the main pointer |
| Main pointer | Shows the reading on the graduated dial |
| Revolution counter | Counts full turns of the main pointer |
| Bezel | Rotates the dial face to set zero |
| Tolerance markers | Mark upper and lower limits on the dial |
| Lifting lever or cap | Raises the plunger without touching the dial |
The revolution counter on a dial gauge records how many full turns the main pointer completes.
What Are the Types of Dial Gauges?
Dial gauges fall into two broad families by spindle motion.
- Plunger dial gauge — uses a spindle that moves in a straight line; suits open, in-line measurement.
- Lever dial gauge — uses a pivoting contact arm; reaches tight or angled points that a plunger cannot.
- Analog dial gauge — uses a graduated dial for direct visual reading.
- Digital dial indicator — shows readings on a display and can output data electronically.
Explore Mitutoyo Plunger Dial Indicators and Lever Dial Test Indicators available at BTSA.

Lever dial test indicators suit tight spaces where a plunger indicator cannot reach the surface. Plunger dial indicators move along their axis and suit height and runout checks.
What Is the Least Count of a Dial Gauge?
Least count defines the resolution of the instrument. A typical metric dial gauge reads to 0.01 mm.
Finer models exist for high-precision work. The value is fixed by the gear ratio and dial graduations.
Read the value stamped on the dial face before measuring. Specific ranges and graduations vary by model.
Where Are Dial Gauges Used?
Dial gauges check runout on shafts and spindles. They verify flatness and parallelism on machined faces. They support comparative gauging when mounted on a stand and confirm machine setup and tool alignment.
- Automotive component inspection
- Bearing and shaft runout measurement
- Machine tool alignment and setup
- General manufacturing quality control
Dial gauges are widely used to check runout, flatness, parallelism and machine alignment.
Is a dial gauge an absolute or comparative instrument?
A dial gauge is mainly a comparative instrument. It shows the difference between a part and a reference, such as a gauge block or master part, after zero is set on that reference. Digital indicators can display absolute values within their travel, but most inspection use is still comparative.
A dial gauge is a comparative instrument that reads deviation from a zeroed reference surface.
How Do You Use a Dial Gauge Correctly?
- Mount the gauge rigidly on a stand or fixture. A stable base reduces error from vibration and deflection.
- Bring the contact point square to the surface.
- Set zero against a master or reference surface.
- Move the part or probe and read the deviation.
- Lift the spindle gently to avoid shock to the mechanism.
Cosine error occurs when a dial indicator contact point is not perpendicular to the measured surface. Dial gauges should be calibrated against traceable standards to keep inspection results valid.
How do you use a dial gauge as a comparator?
- Mount the indicator on a rigid comparator stand over a flat base.
- Set the plunger on a master or gauge block stack of the nominal size.
- Rotate the bezel to zero.
- Replace the master with the part and read the deviation.
- Set the tolerance markers to speed up pass and fail checks.
Mounting a dial gauge on a rigid comparator stand reduces errors from stand deflection. Tolerance markers on the bezel let operators judge pass or fail without calculating each reading.
Frequently Asked Questions
What is a dial gauge used for?
It measures small variation such as runout, flatness and dimensional deviation against a reference. It is widely used in quality control, toolrooms, automotive and bearing manufacturing.
What is the least count of a dial gauge?
A common metric dial gauge reads to 0.01 mm per division. Always confirm the value stamped on the instrument face.
What is the difference between a dial gauge and a dial indicator?
The terms are used interchangeably. Both describe a comparative gauge with a graduated circular dial.
What is the difference between plunger and lever dial gauges?
A plunger gauge moves in a straight line and suits open, in-line measurement. A lever gauge uses a pivoting arm to reach tight or angled points a plunger cannot access.
Does a dial gauge measure absolute size?
No. It measures variation against a set zero or master reference, not the full dimension.
Do dial gauges need calibration?
Yes. Periodic calibration against traceable standards maintains accuracy. BTSA can support calibration requirements based on your instrument and application.
What are the main parts of a dial gauge?
The plunger, contact point, stem, rack and pinion, gear train, main pointer, revolution counter and bezel are the main parts.
What is a dial comparator?
A dial comparator is a dial gauge mounted on a rigid stand with a base. It compares parts against a master of known size.
Related resources
- dial gauge calibration
- NABL calibration
- Mitutoyo measuring instruments
- dial indicator comparator stand
- how to use a lever dial gauge
- cosine error in dial gauges
🔍 Explore Dial Gauges at BTSA | Request a Quote
Browse Mitutoyo dial indicators | Request a quote | Book dial gauge calibration